Salteraa
Salteraa
Salteraa
Salteraa

ZLD to ZLV · powered by MS³-BriMax

Ensuring water and its resources for generations to come.

Salteraa helps the world's water-intensive industries reduce, recover and renew what they use. Our patented MS³-BriMax platform turns industrial effluent into recovered water and saleable salts — building a circular industrial future.

Recover more water Valorise salt resources Reduce energy Reduce carbon emissions Eliminate waste Reduce Opex

Patented technology · IIT Madras validated · CPCB/TNPCB endorsed · Commercially Proven

Our approach

Holistic approach, from effluent to product

Every site presents its own complex brine chemistry. We start from the whole system — upstream and downstream — and engineer the route that recovers the most value from every stream.

01
Recover

Reclaim up to 99% of water on-site and cut freshwater withdrawal — creating a circular water loop for the whole plant.

02
Valorise

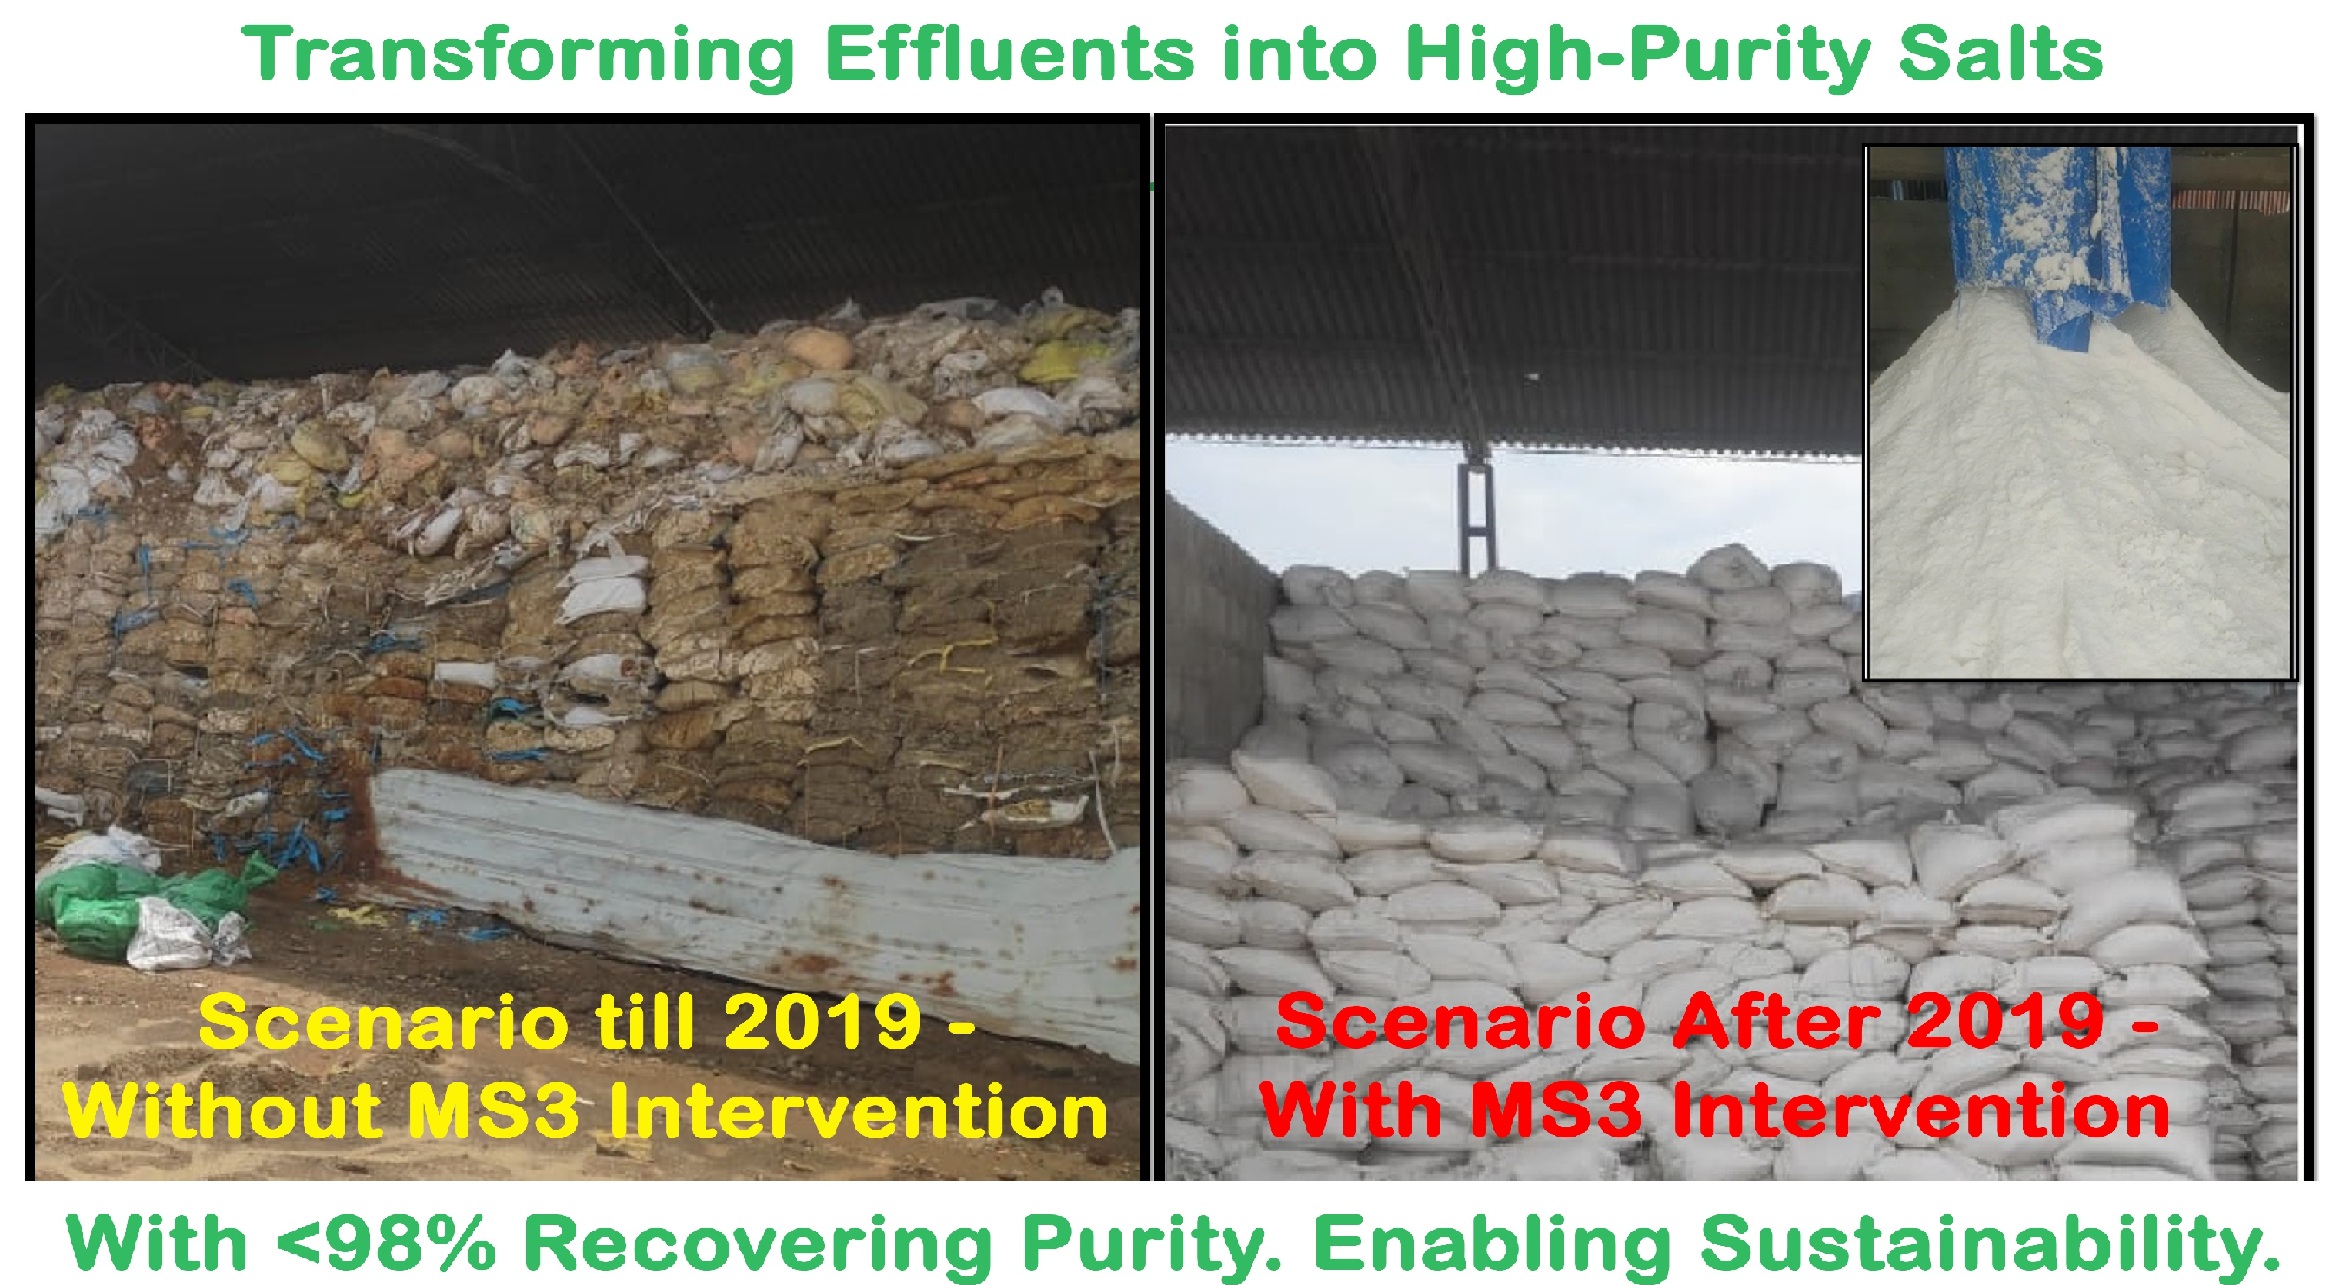
Split mixed brine into individual NaCl and Na₂SO₄ products at 98.5%+ purity — turning waste salt into a valuable commercial resource.

03
Renew

Return recovered salt and recovered water back to industries — closing the industrial loop for a sustainable future.

The measurable difference

Designed for Quantum Leaps, Not Small Steps.

99%
of water recovered for reuse on-site
98.5%+
Purity of each recovered salt stream
60%
Lower thermal evaporation load versus conventional ZLD
35%
Lower carbon footprint through reduced energy consumption and haulage

Compared with a conventional UHPRO + MVRE + ATFD Zero Liquid Discharge process operating on the same feed.

Technology Portfolio

A proprietary stack across the brine value chain

Designed and engineered in-house — separation, concentration, crystallization and the membranes inside them. One accountable technology partner, end to end.

Selective Separation

MS³ Mixed-Salt Separation

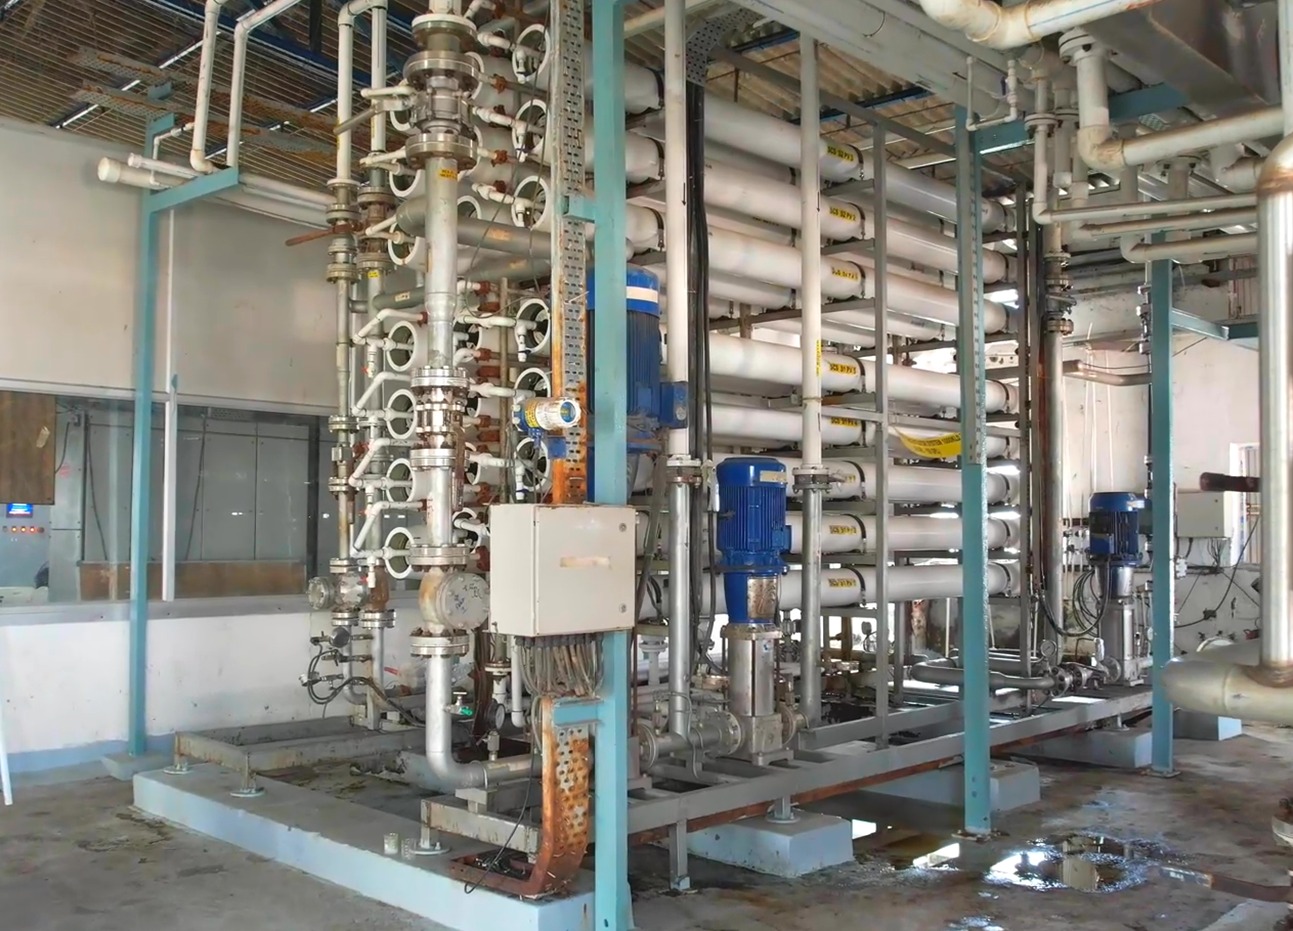
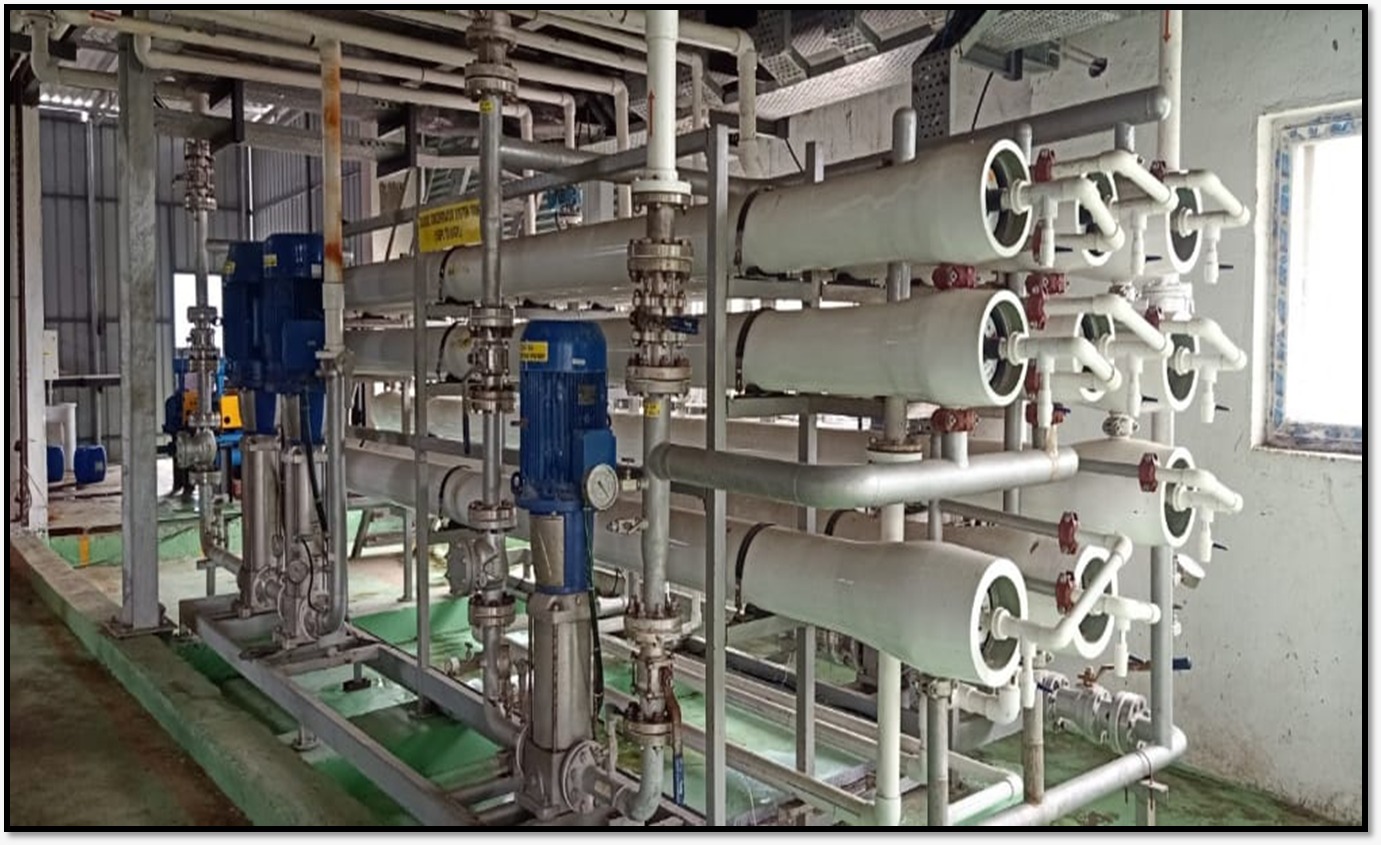
The patented core technology that separates mixed NaCl and Na₂SO₄ streams before the thermal stage, reducing energy consumption and increasing resource recovery.

Non-Thermal Concentration

BriMax Brine Concentration

Concentrates NaCl to approximately 18–22% at around 35°C without boiling, reducing evaporation duty by nearly 60%.

Proprietary Membranes

MS³ Saltionic Membranes

Three membrane families, 105 sector-specific grades, all designed and manufactured by Salteraa.

Thermal Polishing

Crystallization System

Final polishing stage that produces ≥99.5% pure salt crystals with significantly lower thermal energy.

Common Salt Facility

Salt Valorisation Hub

Converts industrial mixed waste salt into reusable commercial-grade products, minimizing landfill disposal.

Delivery Models

EPC · BOOT · O&M

Standardized systems from 100–1000 KLD delivered through EPC, BOOT and long-term Operation & Maintenance services.

Inside the Platform → Products & Membranes →

Why Salteraa

A True Sustainable Solution Company

We Own Our Core

Unlike conventional solution providers, Salteraa owns its patented technology, ensuring continuous innovation, faster deployment and complete accountability.

Commercially Proven

IIT Madras validated, CPCB & TNPCB endorsed, successfully operating through live industrial installations.

Tailor-Made Engineering

Every wastewater stream is unique. We engineer customized recovery systems instead of relying on standard catalogue solutions.

Circular Economy

We don't stop with Zero Liquid Discharge. We convert industrial waste into reusable water, commercial salts and sustainable value.

"Turning industrial wastewater into valuable resources for a cleaner tomorrow."

— Salteraa MS³-BriMax Platform

Industries We Serve

Solutions for Every Water-Intensive Industry

Our patented MS³-BriMax platform supports industries seeking sustainable water management, resource recovery and Zero Liquid Discharge solutions.

🏭

Textile

Water recovery, salt recovery, ZLD optimization and energy reduction.

🧪

Tannery

Sustainable treatment for high TDS wastewater with maximum resource recovery.

💊

Pharmaceutical

Advanced treatment and reuse solutions for complex industrial effluents.

⚗️

Chemical

Recover valuable salts, reduce operating costs and achieve regulatory compliance.

🥛

Food Processing

Efficient wastewater treatment with maximum water reuse.

📄

Paper & Pulp

Lower freshwater demand, recover process water and reduce environmental impact.

Power

Sustainable wastewater management for thermal and industrial power plants.

💧

Electronics & Others

Customized water recovery solutions for every industrial application.

Talk to Our Experts →

Global Presence

Rooted in India, Connected Worldwide

Salteraa collaborates with technology partners, engineering organizations and industries across the globe to deliver sustainable water management and Zero Liquid Discharge solutions.

Ahmedabad, India
Headquarters · Engineering

Corporate headquarters, technology development, research and engineering.

Chennai, India
Operations · Delivery

Project execution, customer support and regional operations.

Middle East & South East Asia
Expansion Roadmap

Expanding strategic partnerships to serve water-intensive industries across international markets.

Strategic Partnerships

USA

Global technology collaboration for EPC and BOOT projects.

EUROPE

Environmental technology and sustainability partnerships.

INDIA

Nationwide engineering, procurement and construction support.

GLOBAL

Supporting industries through innovation, sustainability and resource recovery.

Ready to Transform Your Water Management?

Let's build a sustainable future together.

Whether you're planning a new Zero Liquid Discharge system, upgrading an existing plant, or exploring resource recovery opportunities, our experts are here to help.

Home · About

About Salteraa

Engineering a sustainable future through water innovation

Water is one of the world's most valuable natural resources. We help industries treat it as one — recovering water, salts and chemicals from effluent that others send to landfill.

Who we are

A deeptech water company built on a patented core

Salteraa combines innovation, scientific expertise and practical engineering to solve some of the toughest industrial water-treatment problems. Our patented Mixed-Salt Selective Separation (MS³) technology lets industries recover valuable resources from wastewater while reducing environmental impact.

Our solutions help clients recover high-purity water, salts and chemicals, reduce mixed-salt generation, improve plant efficiency, cut carbon emissions and support sustainable Zero Liquid Discharge operations — designed to lower treatment cost and create long-term environmental and economic value.

31+ & 21+
YEARS OF ZLD EXPERIENCE ACROSS THE FOUNDING TEAM
Patented
GRANTED · OWNED IN-HOUSE
2 cities
AHMEDABAD & CHENNAI · NATIONWIDE EXECUTION

Our vision

Responsible water management, made profitable

We are committed to transforming industrial wastewater into valuable resources. By combining scientific innovation with practical engineering, we enable industries to reduce operational costs, improve sustainability and create long-term value — turning compliance from a cost center into a circular, resource-recovery advantage.

Why work with us

A self-reliant, full-stack technology partner

Owned IP

We own separation, concentration and crystallization — no dependence on a competitor's core technology.

Proven

Validated at IIT Madras, endorsed by CPCB, and backed by a multi-year live operating plant.

Efficient

Selective separation cuts thermal load, energy and CO₂ — lower opex for every plant we build.

Circular

Recovered salts and water return to industry as product — near-zero landfill, real revenue.

Leadership

The inventors and operators behind the platform

Sandip Patel — Founder & CEO

31+ years in ZLD, part of the team behind an early global ZLD plant in brine concentration and industrial water. Leads commercial strategy, partnerships and new-technology development.

T. Gopinath — Founder & CTO

21+ years in ZLD and inventor of the patented MS³ technology. Drives core R&D, the MS³-BriMax technology roadmap, plant operations and process design.

Group & partners

Delivery muscle across India — and beyond

Aquarius H2O Dynamics

Ahmedabad-based execution arm delivering engineering, projects and plant build-out across western India.

ICFCS · Chennai

Incompressible Fluid Control System Pvt. Ltd — Chennai operations, prequalifications and southern-India delivery.

Technology Partner USA
Global water-technology major

Pairing MS³ with a global platform for independent validation and bidding scale on large EPC/BOOT projects.

Delivery & Finance Partner GERMANY
Global environmental major · 30+ countries

Market access, O&M capability and project financing for build-own-operate plants without diluting equity.

Execution Partner INDIA
NSE-listed water EPC

Government prequalifications, a CETP/STP client base and nationwide execution scale for MS³-BriMax roll-out.

Work with a team that owns its technology

Whether you're a plant operator, a CETP cluster or a delivery partner — let's talk about what selective separation can do for your effluent.

Get in touch →

Home · Technology

The MS³-BriMax platform

Selective separation, not brute-force evaporation

We split mixed-salt brine into clean water and individual, saleable salts — at the RO feed and/or reject stage, before the expensive thermal step. Less energy, less waste, more value.

Why conventional ZLD struggles

The mixed-salt bottleneck

Zero Liquid Discharge is mandated for textiles, tanneries, chemicals, power , Paper, Pharma and electronics — but the conventional route is brutal on opex and energy, and it ends in dead-end waste.

Energy-heavy thermal route

Thermal MVRE / MEE routes cost 2–4× conventional treatment and can burn 50–80 kWh per m³ — a cost center, not an asset.

Hazardous mixed salt

Evaporator mixed salt is CPCB-classified hazardous waste — costly TSDF disposal, perpetual liability and zero value.

Our answer

Separate the salts,Shrink the thermal load, crystallize them, Sale them. Recover the water.

How it works

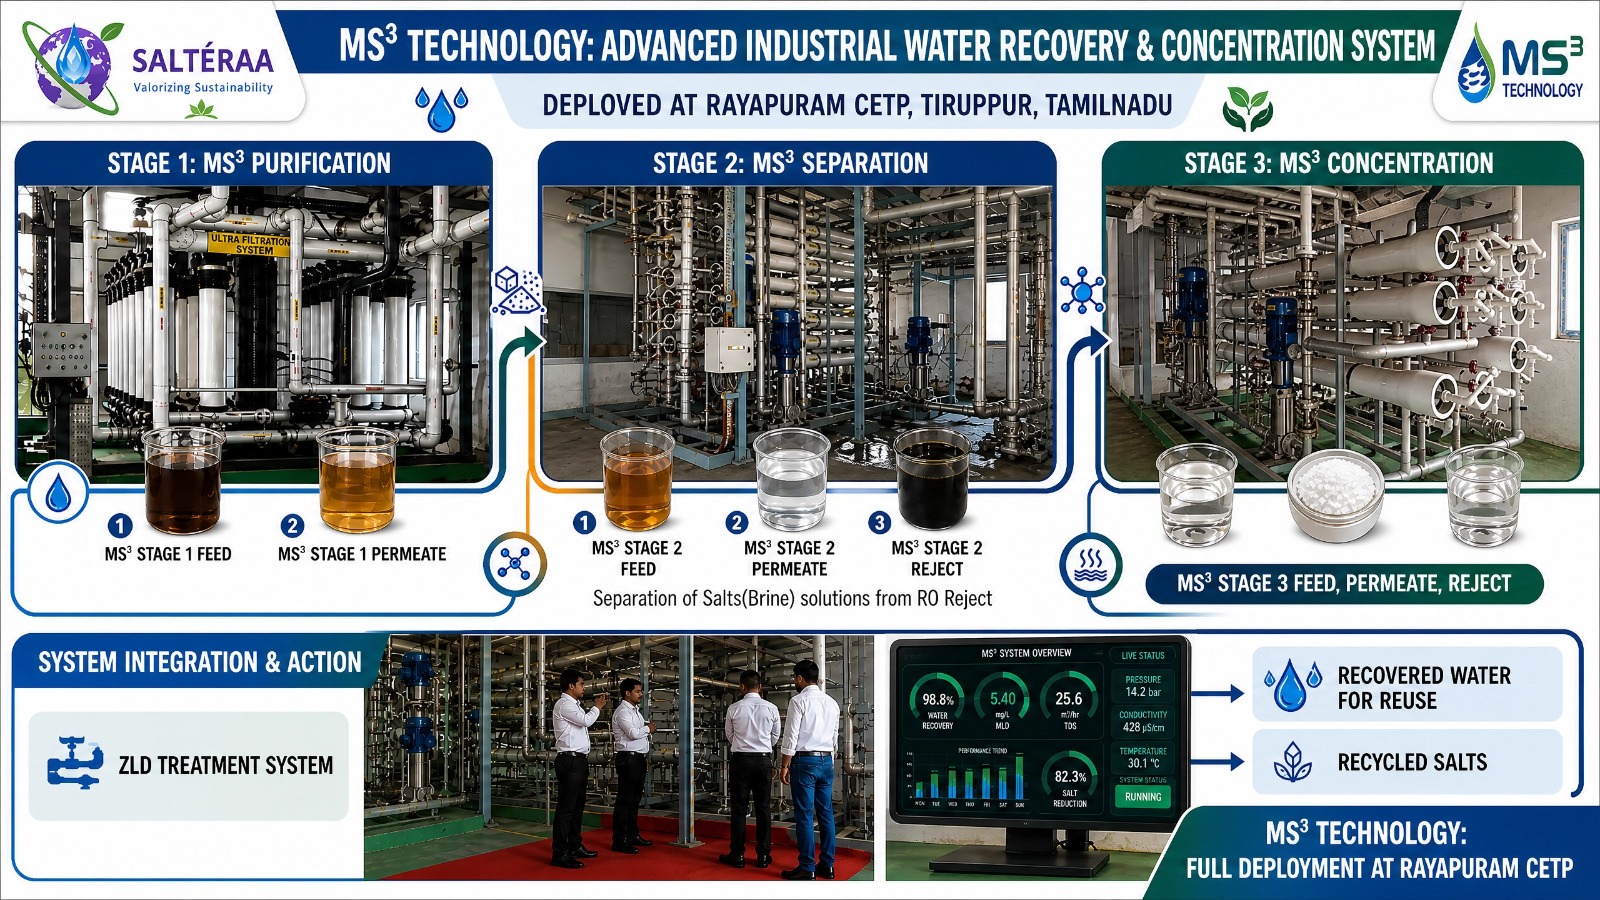
The MS³-BriMax process, step by step

A membrane-led train that does the separation work upstream, leaving only a small polishing duty for the crystallizer.

1

RO reject in

~5-6% TDS mixed NaCl + Na₂SO₄ brine with other impurities enters the train.

2

Pretreatment

Hardness, silica and organics are polished out to protect the selective membranes as required.

3

MS³ selective separation

The patented MS³ step splits the brine into clean NaCl (8–12%) and Na₂SO₄ (~18%) streams.

4

BriMax concentration

Non-thermal concentration to a ~18–22% NaCl stream at ~35 °C — no boiling required.

5

Thermal — polishing only

Final crystallization runs as a light polishing duty, with ~60% lower evaporation load.

6

Products out

NaCl 98.5%+ and Na₂SO₄ 98.5%+ recovered as saleable salts, plus reusable water.

Process route comparison

Two routes, two outcomes

Same RO reject in. One route sells the salt; the other buries it. Here's the difference on the same feed.

MS³-BriMax ZLV

Zero liquid & valorization
WASTE → WEALTH

Pretreatment

Hardness, silica & organics polishing.

MS³ selective separation · patented

Clean NaCl (8–12%) & Na₂SO₄ (18%) streams.

BriMax concentration

Non-thermal to ~18–22% NaCl at ~35 °C.

Thermal — polishing duty only

~60% lower evaporation load.

Two saleable salts + recovered waterOfftake-backed · circular · near-zero disposal.

UHPRO + MVRE ZLD

Conventional membrane–thermal train
WASTE → LANDFILL

Pretreatment

Critical hardness & silica control near saturation.

UHPRO — ultra-high-pressure RO

~110 bar to ~8.5% TDS · salts stay mixed · frequent CIP.

MVRE — full crystallization

Evaporates ~8.5% → crystals · highest-energy step.

Mixed waste salt

Co-crystallized NaCl + Na₂SO₄ · unsaleable · hazardous.

Mixed hazardous solid to landfillPerpetual disposal cost · long-term liability.
Route A · MS³-BriMax-Crystallizer ZLVRoute B · UHPRO + MVRE/MEE ZLD
Salt fateTwo separated, marketable productsMixed hazardous solid — dump-only
Salt purity98.5%+ each streamUnsaleable mixture
Evaporation load~60% lower · non-thermal concentrationFull thermal duty to crystals
Energy & CO₂~35% lower footprintHigher · thermal duty + haulage
DisposalNear-zero landfillPerpetual TSDF fees + transport
OutcomeZero Liquid & ValorizationZLD only · a solid-waste problem

Technology moat

A self-reliant, full-stack platform

Most players license their core technology from global specialists. We own ours — selective separation, non-thermal concentration and crystallization — so we capture the full value chain, and clients get one accountable technology partner.

Granted patent · Mixed-Salt Selective Separation & Concentration for Industrial Effluent & ZLD

Granted patent, owned in-house

The granted patent sits with the company — the defensible core of the platform.

Trade-secret process know-how

Operating data and process design refined on a multi-year live plant.

Proprietary membranes

MS³ Saltionic membranes — the consumable that keeps every plant on our stack.

Productized packages

Standardized systems from 100 to 1,000 KLD for repeatable, fast delivery.

See the products & membranes →

Home · Group of Companies

Our Group of Companies

Our Group of Companies

Our Group of Companies brings together specialized expertise across the complete water and wastewater management value chain. With a strong commitment to sustainability, innovation, and environmental stewardship, we provide integrated solutions that help industries achieve regulatory compliance, optimize resources, and move toward a circular economy.

Our Combined Capabilities

End-to-End Water & Wastewater Solutions

  • Water and Wastewater Treatment Plants (WTP & WWTP)
  • Common Effluent Treatment Plants (CETP)
  • Zero Liquid Discharge (ZLD) Systems
  • Industrial Automation, Electrical & Instrumentation Solutions
  • EPC, Design, Engineering, Procurement, Construction, and Commissioning
  • Operation & Maintenance (O&M) Services
  • Process Optimization, Energy Efficiency, and Water Reuse
  • Environmental Consulting, Compliance, and Sustainability Solutions

Together, our companies deliver end-to-end solutions for textile, tannery, pharmaceutical, chemical, food processing, power, and other industrial sectors.


By combining advanced technologies with operational excellence, we help customers reduce environmental impact, conserve water, recover valuable resources, lower carbon emissions, and build a sustainable future.


Our mission is to be a trusted partner in creating cleaner industries through innovative water management solutions that protect people, preserve nature, and ensure long-term environmental resilience.

Our Companies

Group Companies

Aquarius H2O Dynamics Pvt. Ltd.

Website
www.aquariush20dynamics.in

LinkedIn
Sandip R. Patel

Phone
+91 98253 12346

Incompressible Fluid Control System Pvt. Ltd. (ICFCS)

Website
www.icfcs.in

LinkedIn
T. Gopinath

Phone
+91 98407 55598

Home · Products

Products & Solutions

Patented solutions, designed to recover

Systems that maximize water recovery, recover valuable salts, reduce waste generation and support sustainable ZLD operations across industries — all built on the MS³ core.

Our Solutions

Six ways to put MS³ to work

Concurrent RO Reject Recovery

Recover additional water from reverse-osmosis reject streams using patented Mixed-Salt Selective Separation, reducing discharge and improving plant efficiency.

Industrial ETP-ZLD Solution

A complete Zero Liquid Discharge solution that minimizes mixed-salt generation, recovers reusable brine, lowers operating cost and improves compliance.

Desalination Plant Enhancement

Increase RO permeate recovery, reduce seawater intake, minimize reject volume and improve desalination plant efficiency with MS³ technology.

Desalination ZLD Technology

Recover valuable salts and minerals, reusable water from industrial brine streams while minimizing waste generation and improving resource efficiency.

Wastewater Resource Recovery

Convert industrial wastewater into reusable resources by recovering clean water, valuable chemicals and salts using advanced MS³ technology.

Mixed Salt Valorization

Convert CPCB-classified mixed waste salt into separated, saleable NaCl and Na₂SO₄ — recycling process resources and cutting landfill.

MS³ Saltionic membranes

The consumable inside the moat

Every MS³-BriMax plant runs on membranes designed and owned by Salteraa — not bought from a competitor's catalog. Three families, one form factor, 105 sector-tuned grades.

Three families · 1020-G1 form factor

UF

FOS · UF

Pretreatment shield — solids, organics & fouling control (8 grades per sector).

NF

SSRM · NF

The selective core — splits NaCl from Na₂SO₄ at >98.5% purity (5 grades per sector).

RO

HSC · RO · BriMax

High-salinity concentration to 18–22% for reuse or crystallizer feed (2 grades per sector).

>98.5%
STREAM PURITY · ≥99.5% CRYSTALS
60%
EVAPORATION LOAD REDUCTION
105 models
7 SECTORS · SECTOR-TUNED GRADES

No third-party membrane dependence — full-stack margin capture, and every installed plant becomes recurring replacement supply.

Not sure which solution fits your stream?

Send us your effluent profile and target capacity — we'll recommend the right configuration and membrane grades.

Request a recommendation →
×

Home · Sectors

Industries we serve

One platform, seven high-salinity sectors

Wherever ZLD is mandated and brine is complex, selective separation turns a compliance burden into recovered water and saleable salt.

Textiles

Dye-house and CETP high-TDS effluent — recover water and split mixed salt into reusable NaCl and Na₂SO₄ instead of landfilling it.

Tannery

Salt-heavy, chloride-rich streams handled at source — reducing hazardous mixed-salt generation and disposal liability.

Desalination

Lift permeate recovery, cut seawater intake and shrink reject volume — turning brine into recoverable product.

Pulp & Paper

High-volume process water recovered and recycled, lowering freshwater draw and effluent load.

Chlor-Alkali

Recovered membrane-grade NaCl returns as feed — a closed loop back to the industry that produced the effluent.

Pharma

Complex, regulated effluent with strict discharge norms — compliant ZLD with resource recovery built in.

Oil & Gas

Produced water and high-salinity streams concentrated and separated for reuse and safe handling.

New-wave demand

Solar PV, electronics and gigafactory build-outs are creating fresh high-purity water and brine challenges — squarely in our range.

Talk to us →

Every mandated plant is a recovery opportunity

Tell us your sector and effluent profile — we'll map the water and salt you could be recovering.

Start a conversation →

Home · Sustainability

From ZLD to ZLV

Closing the loop: hazardous waste in, pure product out for sale

Hazardous evaporator salt transformed into membrane-grade salt for circular industrial reuse.

The closed loop

From Hazardous Waste to Circular Resource Recovery

Effluent in

All sector & ETP high-TDS streams. Hazardous mixed salt eliminated — safe, compliant handling.

MS³-BriMax-Crystalizer

Selective separation → NaCl + Na2SO4 + water. Membrane-grade NaCL salt meets chlor-alkali brine specifications & Industrial grade .

Salt out

NaCL to Chlor-alkali feed → caustic soda / soda ash. Caustic returns to the same industries that generated the effluent.

99%
Water reuse on-site
−35%
Lower CO₂ footprint
~95%
Diverted from landfill (via CSVF)
Near-zero
Landfill on Route A

Cluster infrastructure

Common Salt Valorisation Facility (CSVF)

A government-permitted, cluster-level hub that replaces TSDF landfilling — waste salt in, saleable salts out. One facility serves an entire industrial estate.

The same tonne is handled once and put back to productive use — clusters cut disposal cost and long-term liability.

Enablers: SPCB / CPCB authorisation under HWM Rules 2016 · state policy for co-processing & utilisation of waste salt · cluster / ETP partnership.
1

Cluster industries

Waste salt & RO-reject brine handed over officially, under proper authorisation.

2

CSVF processing

patented MS³-BriMax selective separation under SPCB-authorised intake.

3

Pure salts sold

NaCl → chlor-alkali · Na₂SO₄ → glass & detergents, under offtake arrangements.

4

Minimal residue

Only a small non-recoverable fraction goes to secure landfill — the rest is diverted.

Why it matters

Circular economy, made bankable

Lower carbon

Selective separation cuts thermal duty and haulage — up to 35% lower CO₂ versus brute-force thermal ZLD.

Full compliance

HWM Rules 2016 compliance with an audit trail — clusters cut landfill liability and can support SDG reporting.

Real value recovered

Water and salt return to industry as product — resource recovery instead of perpetual disposal cost.

Bring a valorization facility to your cluster

Industrial estates and CETPs: let's explore a Common Salt Valorisation Facility that turns your waste salt into recovered product.

Discuss a CSVF →

Home · Contact

Contact us

Let's turn your brine into a closed loop

Tell us about your effluent streams, capacity and compliance goals. Our team will get back to you shortly.

Talk to the Founders

Gopinath gopinath@salteraa.com Founder & CEO · +91 98253 12346
Sandip sandip@salteraa.com Founder & CTO · +91 98407 55598
Salteraa Private Limited Floor No.: 3RD FLOOR, 303,
Suryansh Gateway,
Sardar Patel Ring Road,
Bhadaj, Ahmedabad,
Gandhinagar,
Gujarat - 382722
SALTERAA PRIVATE LIMITED - CHENNAI OFFICE

Second Floor, No.13/24,
East Road,
West CIT Nagar,
Chennai – 600035

Send a Message